Blog
In a field that evolves daily, staying ahead means staying informed.
Explore in-depth articles designed to help you solve complex challenges,
maximize your machine’s ROI.
Stay ahead in a competitive market.

In a field that evolves daily, staying ahead means staying informed.
Explore in-depth articles designed to help you solve complex challenges,
maximize your machine’s ROI.
Stay ahead in a competitive market.
News | Sep-21-2026
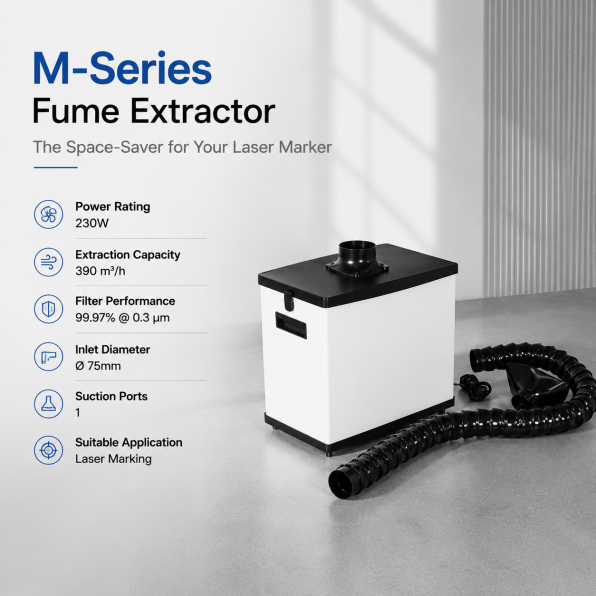
When a CO2 Laser Cutter is used for engraving and cutting, the process can generate smoke, dust, particles, and material-specific fumes that need to be properly managed. A table top fume extractor provides a compact way to capture and filter airborne contaminants close to the processing area, making it particularly useful for small laser workstations, laboratories, educational environments, prototyping spaces, and low-volume production.
For users who do not need a large centralized extraction system, a properly selected tabletop unit can provide a more compact approach to localized fume management.
A table top fume extractor is a compact filtration system designed to capture fumes and particles generated during processes such as laser cutting, laser engraving, soldering, and other small-scale manufacturing operations.
For laser applications, the important specifications are not simply the physical size of the extractor. Airflow, filtration stages, filter type, capture distance, noise level, filter capacity, and compatibility with the processed material all affect performance.
A tabletop extractor is generally most practical when the processing area is relatively small and the source of fumes can be positioned close to the extraction inlet.
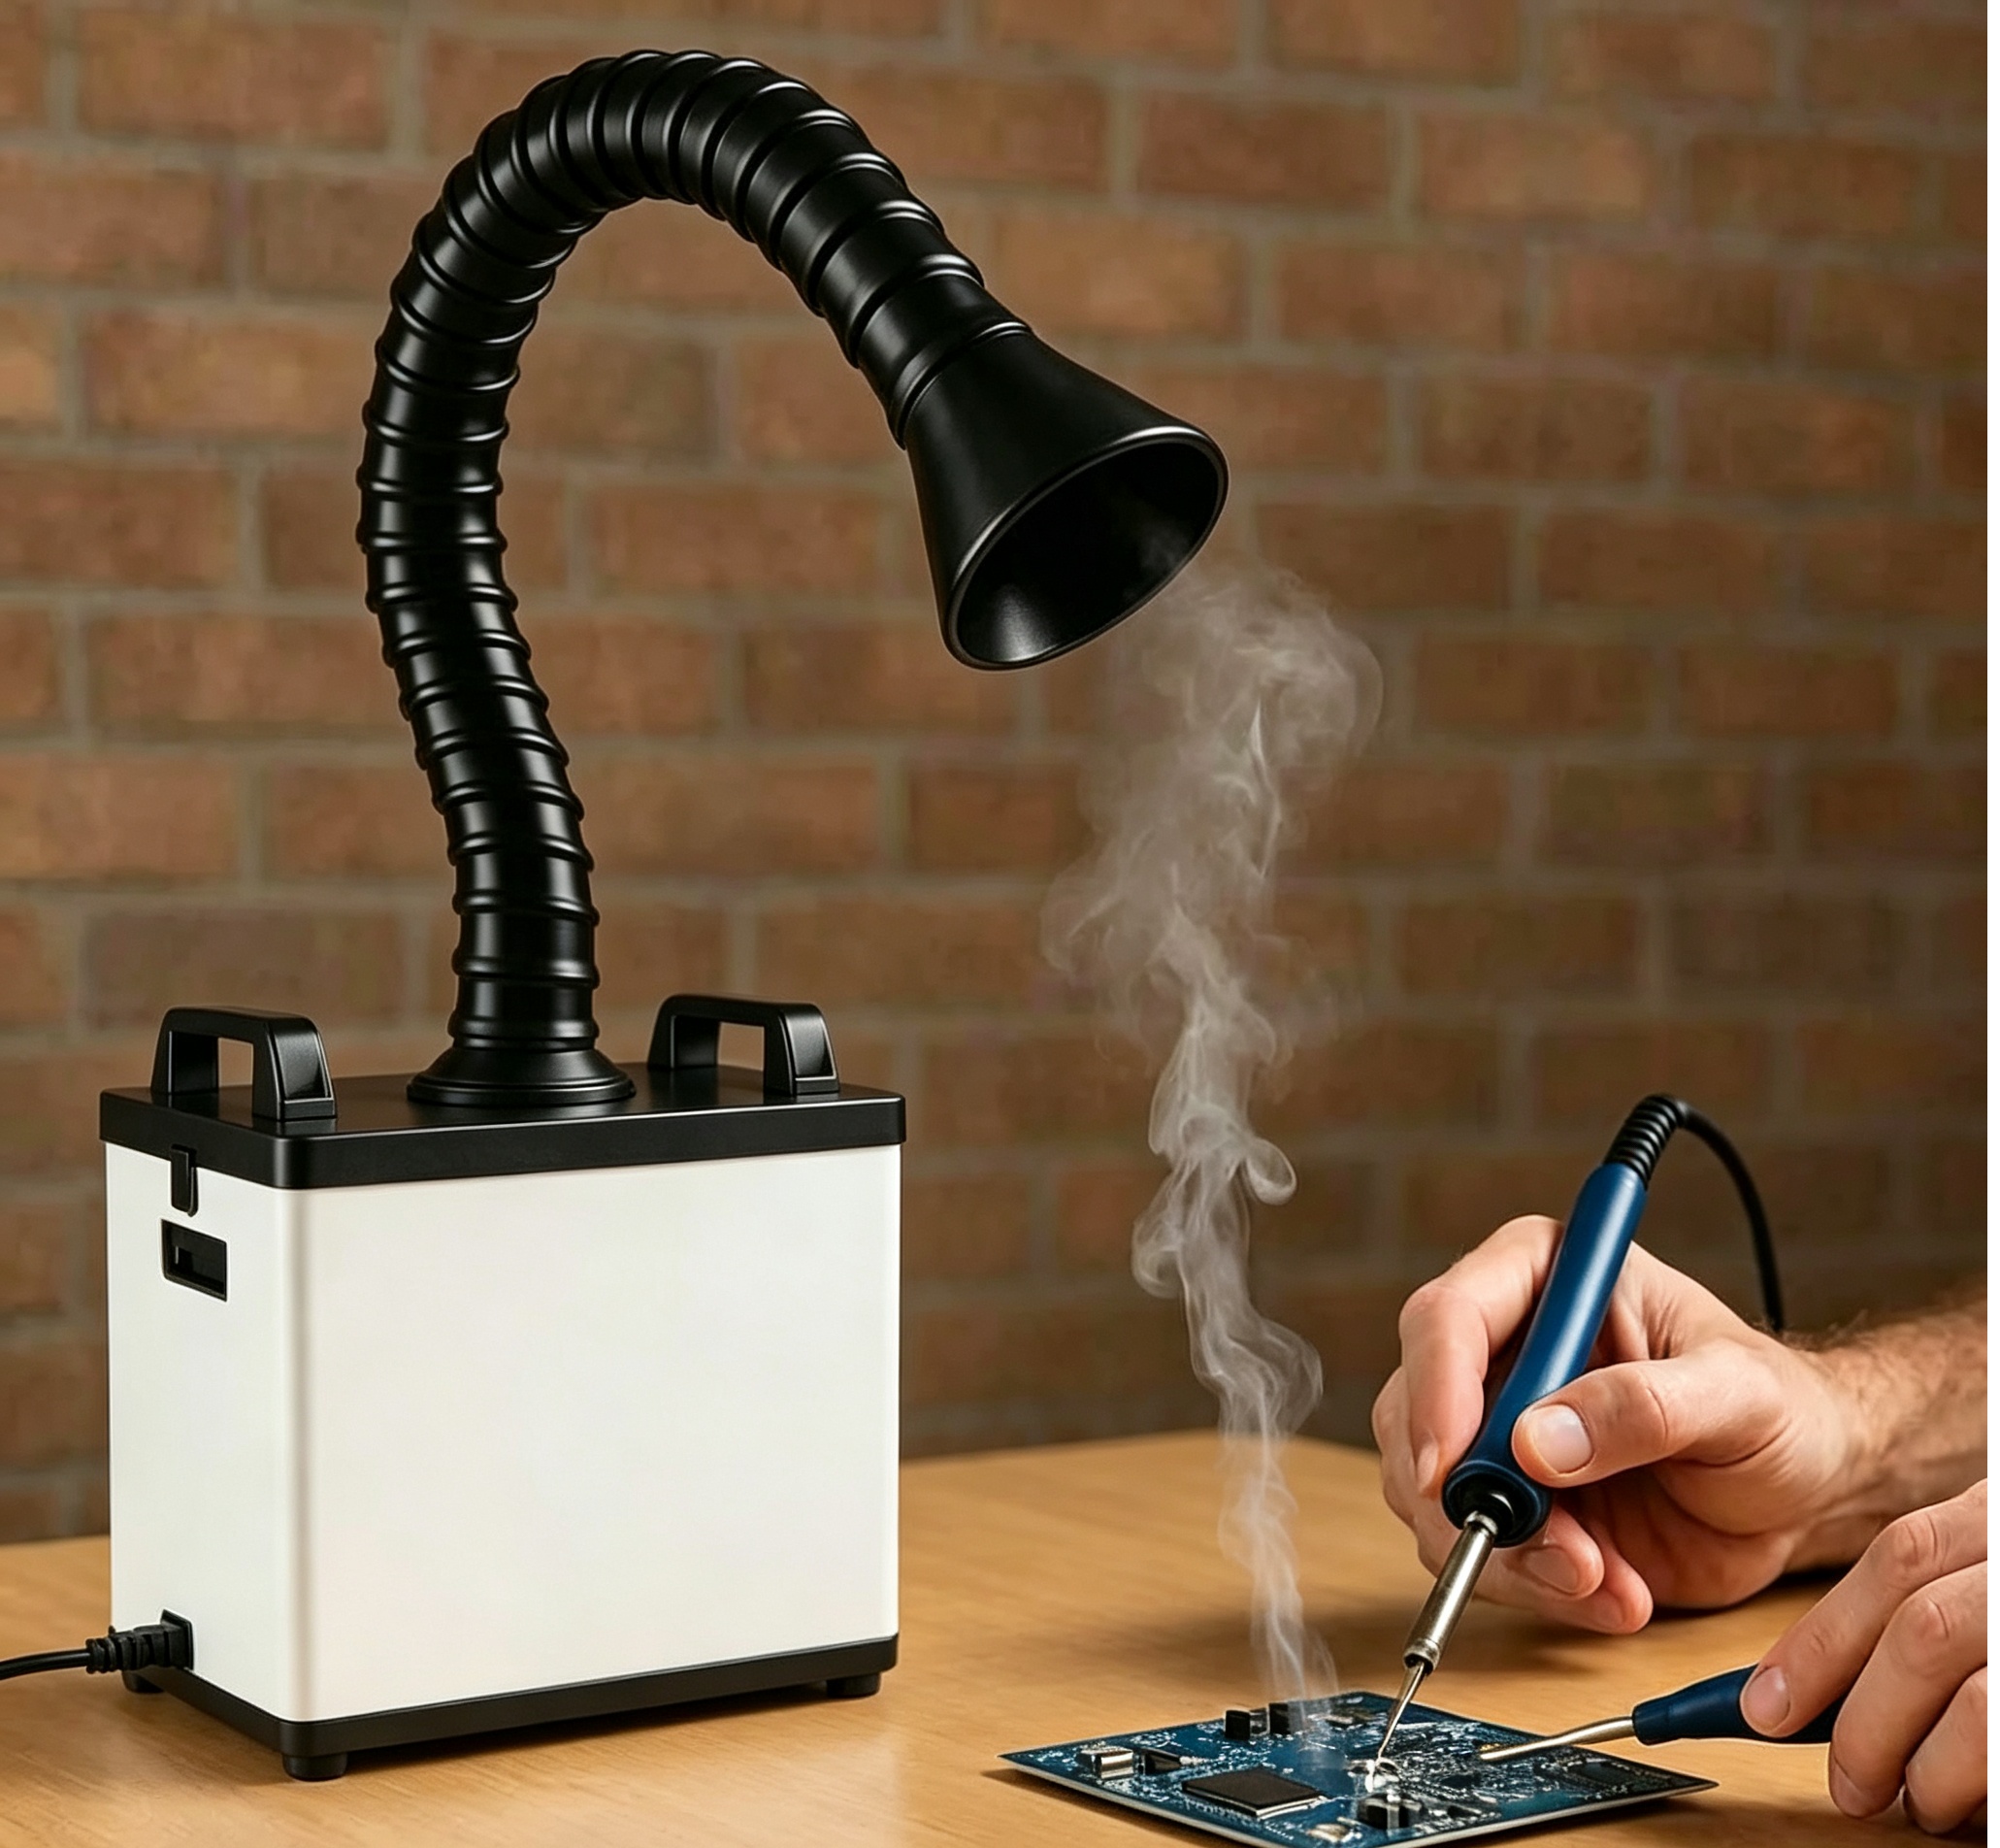
A table top fume extractor is a localized air-cleaning system designed to capture contaminants directly around a workstation.
Instead of attempting to clean the air in an entire room, the system focuses on the source where smoke or fumes are generated.
A typical system uses an extraction fan to draw contaminated air through one or more filtration stages. Depending on the application, these stages may include particulate filtration and activated carbon or other gas-phase filtration media.
For laser engraving, the exact filtration requirements depend heavily on the material being processed.
Wood, acrylic, plastics, coated materials, rubber, leather, and composites can produce very different airborne contaminants when exposed to laser energy. Consequently, a filter system should be selected according to the actual materials and processing conditions rather than simply purchasing the smallest available unit.
Laser cutting and engraving are thermal processes. Material is heated, vaporized, decomposed, or removed by the laser beam.
The resulting airborne contaminants can include fine particles, smoke, and gaseous byproducts.
The extraction system therefore has two important functions.
First, it helps remove contaminants from the immediate processing area. Second, effective extraction can improve visibility around the workpiece and reduce the accumulation of smoke inside the laser enclosure or workstation.
For production environments, extraction can also form part of the overall machine safety and ventilation design.
However, a fume extractor should not be treated as a universal solution for every material. Some materials can release hazardous substances when heated, and those materials may be unsuitable for laser processing regardless of the extraction equipment being used.
The basic airflow path is relatively straightforward.
Contaminated air is captured near the laser processing area and pulled into the extractor by a fan. The air then passes through filtration stages designed to remove different types of contaminants.
A simplified system can be represented as:
Laser processing → Smoke and fumes → Local capture → Particle filtration → Gas filtration → Filtered air
The first filtration stage commonly deals with larger particles and dust. A finer filter can then capture smaller airborne particles, while activated carbon or another suitable adsorption medium can help address certain gaseous contaminants and odors.
The exact configuration varies between extractor designs and applications.
A good tabletop fume extraction system is normally designed around multiple filtration functions rather than relying on one filter.
| Filter Stage | Primary Function | Relevance to Laser Processing |
| Pre-filter | Captures larger particles | Helps protect downstream filters |
| Fine particle filter | Captures smaller particles | Important for laser-generated particulate matter |
| HEPA filter | High-efficiency particle filtration | Useful where fine particles need high-efficiency filtration |
| Activated carbon | Adsorbs certain gases and odors | Relevant for many organic materials |
| Specialized media | Targets specific contaminants | Depends on the material and process |
Not every application requires every filtration stage.
For example, particle filtration alone does not address every gaseous compound, while activated carbon should not be considered a replacement for a high-efficiency particle filter.
The filtration architecture should therefore match the contamination profile produced by the material.
These systems solve different problems.
Room ventilation exchanges or dilutes air throughout a larger space. Local fume extraction attempts to capture contaminants near their source before they disperse.
| Factor | Table Top Fume Extractor | General Room Ventilation |
| Primary purpose | Localized contaminant capture | Overall air exchange |
| Capture location | Near processing source | Throughout room |
| Installation | Usually compact | Building-level or room-level |
| Portability | Generally high | Low |
| Suitable for small workstations | Yes | Not specifically designed for this |
| Filtered air | Depends on system | Depends on HVAC design |
| Source capture | Strong when positioned correctly | Limited |
| Larger production areas | May require multiple systems | More appropriate as part of facility ventilation |
In a properly designed workshop, local extraction and room ventilation can complement each other.
A tabletop extractor should not automatically be viewed as a substitute for required facility ventilation or an engineered exhaust system.
Material compatibility is one of the most important considerations.
For common laser applications, users may process wood, plywood, MDF, acrylic, paper, cardboard, textiles, leather, and certain plastics.
However, the fact that a material can physically be cut by a laser does not mean that every material is suitable for every extraction system.
PVC and materials containing chlorine, for example, should not be treated as ordinary laser-processing materials because laser heating can generate corrosive and hazardous byproducts.
Likewise, unknown plastics, heavily coated materials, and materials with uncertain chemical compositions should be evaluated carefully before processing.
The extractor needs to be selected after understanding the material, not before.
Airflow is one of the most important specifications, but a larger airflow rating does not automatically mean better extraction.
The required airflow depends on the size of the capture area, enclosure design, extraction hose, inlet geometry, distance from the source, pressure losses, and the amount of smoke generated.
A compact desktop laser workstation may have very different extraction requirements from a larger enclosed laser cutter.
There is also an important distinction between the manufacturer’s free-air airflow rating and the airflow available when filters, hoses, ducts, and bends create resistance.
As filters become loaded, airflow can also decline.
Therefore, buyers should consider the extractor’s performance under realistic operating conditions rather than comparing only the maximum airflow number.
Filters are consumable components.
As particles accumulate and adsorption media become saturated, the extractor’s performance can decrease. A system that initially provides strong airflow may perform differently after extended use.
For this reason, a professional extraction system should provide a practical way to monitor filter condition.
Maintenance intervals depend on material type, processing frequency, laser power, operating time, and contamination load.
A user cutting plywood for several hours every day may consume filters significantly faster than someone engraving small wooden products for a few minutes at a time.
The cost of replacement filters should therefore be included when calculating the long-term operating cost.
Noise can become particularly noticeable when an extractor is located directly beside an operator.
For schools, design studios, laboratories, offices, and small workshops, acoustic performance may be almost as important as extraction capacity.
A powerful fan running continuously can create a significant amount of background noise. On the other hand, reducing airflow too aggressively to achieve lower noise may compromise capture performance.
The objective is to find an appropriate balance between airflow, filtration resistance, and acoustic performance.
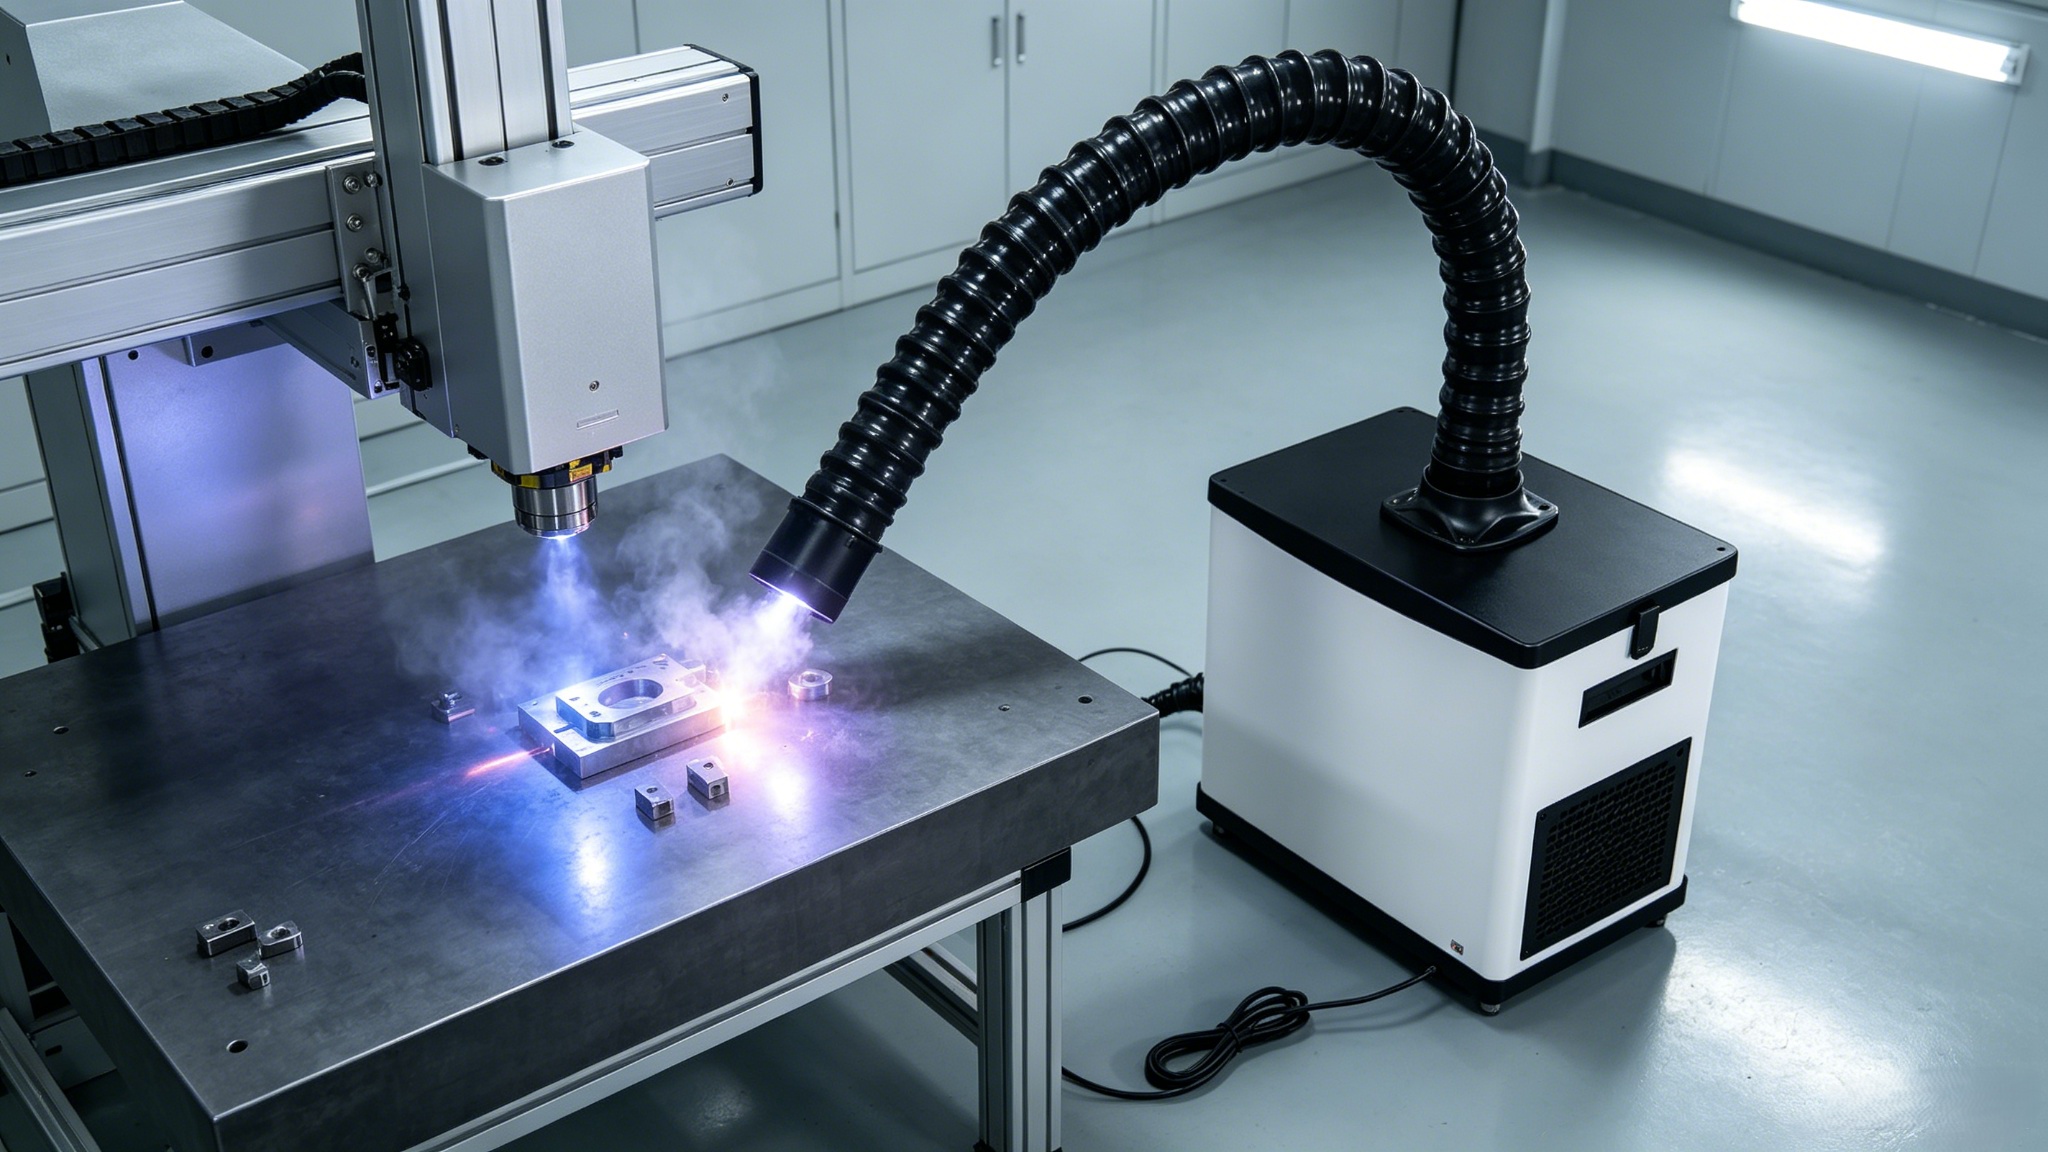
The selection process should begin with the laser application.
Suppose the extractor will be used with a small desktop CO₂ laser for engraving wood and acrylic. The required system would be different from an industrial extractor serving multiple laser processing stations.
The first consideration is therefore the contaminant source.
Next, consider the working enclosure and extraction connection. A well-designed capture path can significantly affect real-world performance.
Then evaluate the filtration stages. Particle filtration and gas-phase filtration solve different problems, so a system intended for laser fumes should be evaluated according to both requirements.
Finally, consider maintenance, filter replacement, noise, footprint, and operating cost.
| Selection Factor | What to Check |
| Airflow | Performance under filter and duct resistance |
| Filtration | Particle and gas-phase filtration requirements |
| Capture method | Distance and connection to the source |
| Filter capacity | Expected service life |
| Noise | Suitability for the working environment |
| Footprint | Available tabletop/workstation space |
| Maintenance | Filter replacement and monitoring |
| Materials | Compatibility with the materials being processed |
| Operating cost | Replacement filters and energy consumption |
Not necessarily.
A filtered tabletop extractor and an externally exhausted system operate differently.
An externally exhausted system removes contaminated air from the workspace and discharges it through a properly designed exhaust route, subject to local building, environmental, and safety requirements.
A filtration system instead captures contaminants and passes the air through its internal filters.
Which approach is appropriate depends on the machine, material, facility, local requirements, and system design.
For larger industrial laser operations, a centralized extraction system may be more suitable than a tabletop unit.
For compact workstations, a self-contained filtration system can offer a practical alternative where its specifications and filtration capabilities are appropriate.
One of the strongest use cases for a table top fume extractor is a compact laser workstation.
Small businesses, makerspaces, schools, laboratories, and prototyping environments may not have the space or infrastructure required for a large industrial extraction installation.
A compact extractor can be positioned close to the laser workstation, minimizing installation requirements while providing localized filtration.
This is particularly useful when the workload consists of short production runs, engraving, prototyping, or customized products.
However, the system should still be sized according to actual processing conditions rather than workstation dimensions alone.
A tabletop fume extractor is used to capture and filter airborne contaminants generated close to a workstation. In laser applications, it can help manage smoke, fine particles, and certain gaseous contaminants produced during cutting and engraving.
Yes, provided that the extractor is appropriately sized and its filtration system is compatible with the materials being processed. The laser enclosure, airflow requirements, filter type, and material characteristics all need to be considered.
A properly designed extraction and filtration system can capture laser-generated smoke and particles. The effectiveness depends on capture position, airflow, filtration efficiency, filter condition, and the material being processed.
Not necessarily. HEPA filtration is designed primarily for high-efficiency particle filtration. Some laser processes also generate gaseous contaminants and odors, which may require an appropriate gas-phase filtration medium such as activated carbon.
There is no universal replacement interval. Filter life depends on the material, laser power, operating hours, contamination load, and filter capacity. Monitoring pressure drop, airflow, filter indicators, or manufacturer-recommended service intervals can help determine when replacement is needed.
That depends on the extractor’s airflow, connection design, operating conditions, and the number of machines running simultaneously. A system designed for one compact workstation should not automatically be assumed to provide sufficient extraction for multiple machines.
A table top fume extractor can provide localized fume and particle management for compact laser cutting and engraving workstations. Its effectiveness depends on much more than the size of the unit.
Airflow under real operating conditions, capture design, filtration stages, filter capacity, material compatibility, maintenance requirements, and operating environment should all be evaluated together.
For users operating a small or desktop CO2 Laser Cutter, a properly matched tabletop filtration system can help create a more controlled processing environment. For larger production facilities or applications with substantial contaminant loads, a dedicated industrial extraction and ventilation solution may be more appropriate.
The most reliable approach is to identify the materials and processing conditions first, then select the extraction technology and filtration configuration around those requirements.
News | Aug-14-2026
News | Jul-3-2026
News | Apr-16-2026