Blog
In a field that evolves daily, staying ahead means staying informed.
Explore in-depth articles designed to help you solve complex challenges,
maximize your machine’s ROI.
Stay ahead in a competitive market.

In a field that evolves daily, staying ahead means staying informed.
Explore in-depth articles designed to help you solve complex challenges,
maximize your machine’s ROI.
Stay ahead in a competitive market.
News | Sep-21-2026
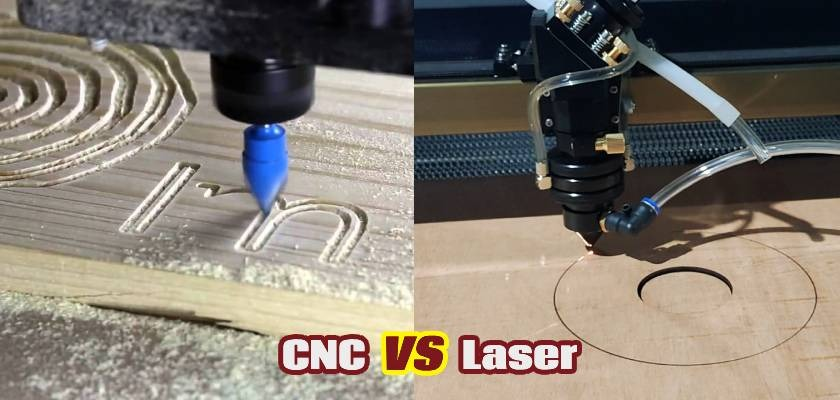
When choosing between a laser cutter or CNC router, the decision should begin with the type of production you actually need rather than the machine’s price or advertised power. A CO2 Laser Cutter can process wood and other non-metal materials through a focused beam, while a CNC router removes material mechanically with a rotating cutting tool. Both technologies are capable of cutting wood, but they create different workflows, edge characteristics, surface effects, and production possibilities.
Choose a laser cutter when your priority is precise digital cutting, detailed engraving, intricate contours, small holes, and frequent design changes.
Choose a CNC router when you primarily need mechanical cutting, deeper material removal, thicker stock processing, or applications that benefit from physical routing tools.
For businesses producing customized wooden products, signage, decorative panels, and detailed designs, a CO₂ laser can combine cutting and engraving in one non-contact process. For heavy-duty woodworking and deeper three-dimensional machining, a CNC router may be more appropriate.
The fundamental difference is how the two machines remove material.
A laser cutter concentrates a high-energy beam onto the workpiece. The material is heated and removed along a programmed path. Since there is no physical cutting tool contacting the material, the machine can follow very small contours without creating mechanical cutting forces.
A CNC router uses a rotating tool to physically cut, mill, or carve the material. The machine moves the cutting tool along programmed X, Y, and Z axes.
This creates two fundamentally different production environments.
Laser cutting is essentially a thermal, non-contact process, while CNC routing is a mechanical material-removal process.
Understanding this distinction makes it much easier to determine which machine fits a particular application.
| Comparison Factor | CO₂ Laser Cutter | CNC Router |
| Processing method | Thermal, non-contact | Mechanical cutting |
| Wood cutting | Excellent for many sheet materials | Excellent |
| Engraving | Highly suitable | Highly suitable |
| Fine details | Excellent | Depends on tool diameter |
| Small internal features | Strong capability | Tool size can become a limitation |
| Physical cutting force | None | Present |
| Tool wear | No cutting bit | Cutting tools wear over time |
| Dust generation | Smoke and fumes | Sawdust and chips |
| Edge appearance | Heat-affected edge | Mechanically cut edge |
| Design changes | Very fast digital changes | Also digital, but tool selection matters |
| Deep 3D machining | Limited | Strong capability |
| Sheet processing | Highly suitable | Highly suitable |
The table shows why neither technology should be treated as a universal replacement for the other.
The better choice depends on what “cutting” means in your production environment.
A laser cutter becomes particularly attractive when the product contains complex two-dimensional geometry.
Consider a wooden sign with small lettering, decorative holes, curved outlines, and an engraved surface pattern. The entire design can be created digitally and sent to the laser system without physically changing a cutting tool.
This makes laser technology useful for businesses that frequently change designs.
Customized gifts are another example. A customer may request a different name, logo, number, or pattern for every order. Because the production information is digital, the operator can modify the file and produce the next design without manufacturing a new physical template.
For this type of workflow, the flexibility of laser processing can be more important than raw cutting depth.
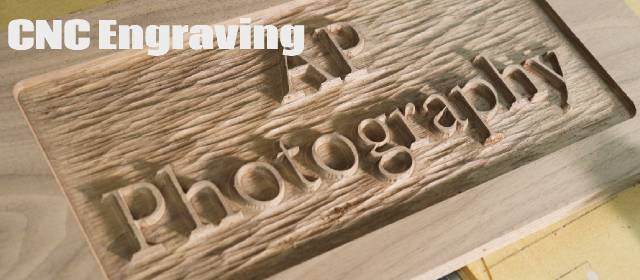
CNC routers have a different strength.
Because the cutting tool physically removes material, CNC systems can perform operations such as deep routing, pocketing, drilling, carving, and three-dimensional machining.
This makes them valuable when the objective goes beyond cutting a flat sheet.
For example, a woodworking manufacturer may need to create a recessed pocket, carve a deep profile, or machine a thick wooden component. These operations are naturally aligned with the mechanical capabilities of a CNC router.
Tool selection also allows the router to adapt to different machining requirements.
The trade-off is that the cutting tool has a physical diameter and must contact the workpiece. Very small internal corners and extremely fine details may therefore require smaller tooling, slower processing, or additional operations.
For intricate sheet designs, the physical geometry of the cutting tool becomes an important consideration.
A CNC router cannot normally create an internal corner smaller than the practical geometry of the cutting bit without additional machining. A laser beam, by comparison, does not have the same mechanical tooling limitation.
This is one reason laser cutting is widely used for decorative wood products, intricate patterns, model components, personalized signage, and small-format parts.
However, precision should not be confused with overall machining capability.
A laser may be highly effective for detailed two-dimensional cutting but is not designed to replace a CNC router for every three-dimensional woodworking operation.
Thickness is another important part of the decision.
CNC routers can mechanically process relatively thick wood by removing material progressively with a cutting tool. Laser systems can also cut substantial wood thicknesses, but the practical limit depends heavily on laser power, material density, moisture, resin, construction, focus, and required edge quality.
For a laser user, increasing thickness often means balancing cutting speed against heat accumulation and edge quality.
For a CNC user, thicker material means considering spindle power, cutting depth per pass, tooling, feed rate, and machine rigidity.
Therefore, asking simply “Which machine cuts thicker wood?” does not provide enough information.
A more useful question is:
“Which technology can process my material at the required thickness, quality, and production speed?”
One of the most important differences between laser cutting and CNC routing is the appearance of the finished edge.
Laser cutting creates a thermally affected edge. Depending on the wood, parameters, and air assistance, the edge may show darkening or carbonization.
CNC routing produces a mechanically machined edge. Its appearance depends on cutter geometry, feed rate, spindle speed, tool condition, and the characteristics of the wood.
For some products, a darker laser edge is part of the desired visual style. For other products, a natural mechanical edge may be preferred.
This is why sample testing is valuable before choosing a production technology.
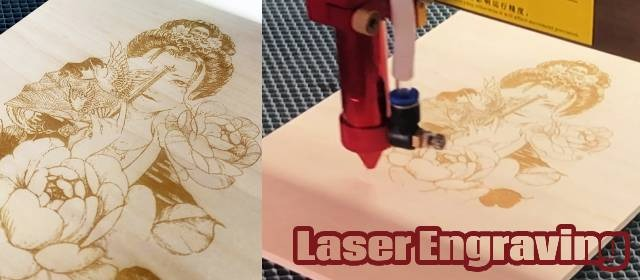
The engraving process is another area where the technologies differ significantly.
A laser can raster or vector engrave a surface by controlling where energy is delivered. This makes it convenient for photographs, logos, fine patterns, text, and variable graphics.
A CNC router engraves by mechanically removing material with a tool. It can create deeper grooves and sculptural effects, but the result depends strongly on cutter geometry and machining strategy.
For shallow decorative engraving and highly variable graphics, laser processing can offer a straightforward digital workflow.
For deeper carving and three-dimensional relief work, CNC routing has a natural advantage.
The workflow should also influence your decision.
With laser cutting, the operator typically moves from digital artwork to machine parameters and then directly to processing. If a customer changes the design, the digital file can be modified without replacing physical tooling.
A CNC router follows a similarly digital workflow, but machining strategy is more closely connected to tool selection, cutting depth, toolpaths, and spindle parameters.
For businesses with hundreds of small design variations, reducing physical setup can be particularly valuable.
For standardized products requiring deeper machining operations, CNC routing may provide more suitable process control.
The following framework can help clarify the decision.
| Your Main Requirement | More Suitable Technology |
| Detailed 2D wood cutting | CO₂ laser |
| Fine decorative patterns | CO₂ laser |
| Personalized signs | CO₂ laser |
| Frequent design changes | CO₂ laser |
| Surface engraving | CO₂ laser |
| Deep carving | CNC router |
| 3D woodworking | CNC router |
| Deep pockets and channels | CNC router |
| Heavy mechanical material removal | CNC router |
| Mixed cutting and detailed engraving | CO₂ laser |
This is not a ranking of the two technologies. They solve different manufacturing problems.
In some workshops, the most practical solution may even be to use both. A laser can handle detailed cutting and engraving, while a CNC router performs deeper machining operations.
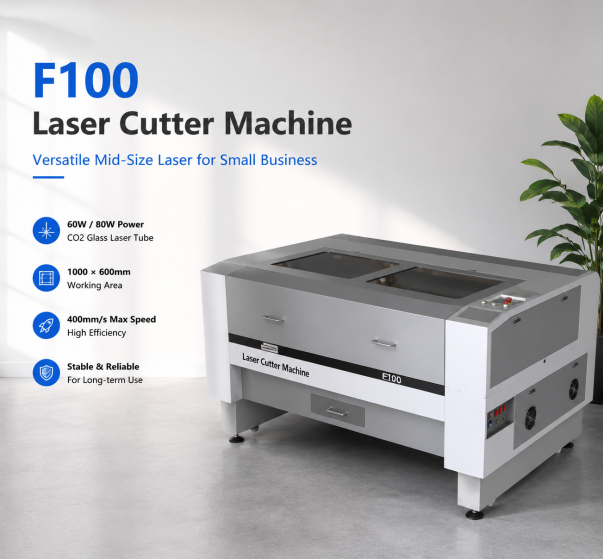
For many wood-processing applications, yes.
MimoWork’s CO₂ laser systems are designed for non-metal materials including wood and wood-based materials, with different machine sizes and power configurations available for different production requirements. Current MimoWork guidance also highlights applications ranging from personalized wooden products and signs to larger decorative and commercial components.
The important point is to match the machine configuration with the material and production process.
A small workshop producing thin decorative parts does not need the same configuration as a manufacturer processing large wooden panels every day.
Related Guide: Best CO2 Laser Engraver for Small Business: A Practical Buying Guide
Neither machine is universally better. A laser cutter is particularly suitable for detailed cutting, engraving, intricate patterns, and digitally customized products. A CNC router is better suited to deeper mechanical machining, carving, pockets, and three-dimensional woodworking.
A CO₂ laser can cut wood, but achievable thickness depends on laser power, wood density, moisture, construction, focus, cutting speed, and the required edge quality. Testing the actual material is recommended before production.
It can. Because laser cutting uses heat, the edge may become darker depending on the material and processing parameters. Air assistance and optimized power and speed settings can help control excessive burning.
Yes. CNC routers can engrave and carve wood by mechanically removing material. They are especially useful when deeper grooves, pockets, or three-dimensional relief are required.
Yes. CO₂ laser systems can combine cutting and engraving within the same digital workflow. This is one of the reasons they are commonly considered for customized wood products and small-batch production.
Start with the products rather than the machine. If your business depends on detailed sheet cutting, personalization, engraving, and frequent design changes, evaluate a CO₂ laser system. If your products require deep carving, heavy material removal, or three-dimensional machining, evaluate a CNC router.
The decision between a laser cutter or CNC router is ultimately a question of manufacturing method.
A CO₂ laser cutter uses concentrated thermal energy to process material without physical contact, making it particularly effective for detailed cutting, engraving, customization, and complex two-dimensional designs.
A CNC router uses mechanical cutting tools and offers strong capabilities for deep machining, carving, pockets, and three-dimensional woodworking.
For businesses focused on digital customization and detailed wood products, laser processing can provide a flexible workflow. For applications centered on deeper mechanical machining, CNC routing offers a different set of capabilities.
Before purchasing either machine, test your actual material, product dimensions, required thickness, design detail, production volume, and finished-edge requirements. That practical comparison will provide a more reliable basis for equipment selection than comparing machine specifications alone.
News | Aug-20-2026