
Quick Answer
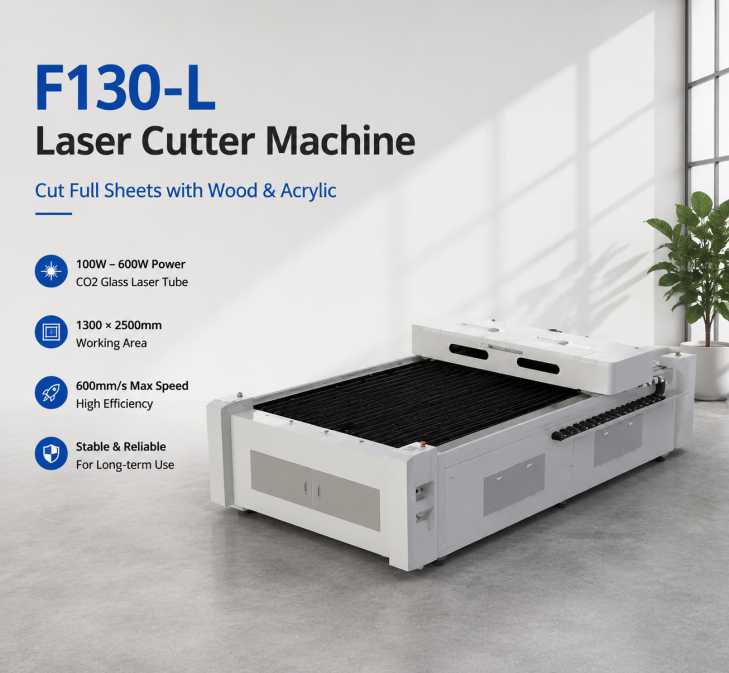
Woodworking businesses increasingly use laser cutting for customized components, decorative panels, signage, and detailed product designs. A CO2 laser cutter for wood can produce intricate shapes without direct contact with the material, making it useful for applications where design flexibility and repeatability matter.
However, cutting performance is not determined by laser power alone. Wood species, board composition, thickness, cutting speed, and extraction conditions all influence the final result. Choosing suitable equipment means evaluating the complete production process rather than focusing on a single machine specification.
What Can a CO2 Laser Cutter Do With Wood?
A CO2 laser cutter can process many wood materials into customized shapes, openings, patterns, and components. Its non-contact cutting process is particularly useful for detailed designs that would be more difficult to produce with conventional cutting tools.
CO2 lasers are widely used for wood processing because wood absorbs their infrared energy effectively. The resulting heat removes material along the cutting path, allowing manufacturers to produce complex contours and repeatable designs.
- Common applications include:
- Decorative panels:Intricate patterns, wall decorations, and interior design elements.
- Wooden signage:Letters, logos, signs, and customized display pieces.
- Furniture components:Decorative inserts, selected structural details, and customized parts.
- Craft and gift products:Personalized ornaments, wooden accessories, and small-batch products.
- Retail displays:Branded wooden displays, product stands, and decorative packaging elements.
For manufacturers, the main advantage is the ability to change cutting designs through digital files without manufacturing dedicated mechanical tooling for every new shape.
Which Wood Materials Can a CO2 Laser Cutter Process?
CO2 laser cutting can be used for solid wood and selected engineered wood products, but different materials do not produce identical results. Their density, moisture, internal structure, and chemical composition influence cutting behavior.
| Wood material | Typical applications | What to evaluate |
| Solid wood | Signs, ornaments, decorative parts, and customized components | Species, grain direction, density, and moisture |
| Plywood | Decorative panels, product components, and customized shapes | Adhesive composition, layer consistency, and edge quality |
| MDF | Signage, decorative panels, and selected furniture components | Binder composition, emissions, and smoke extraction |
| Thin wood sheets and veneer | Decorative inlays, patterns, and detailed designs | Sheet stability, thickness, and material support |
Why Does Material Composition Matter?
Solid wood is a natural material with variations in grain, density, resin, and moisture. These differences can cause uneven cutting or localized darkening.
Engineered boards introduce additional considerations. Plywood contains adhesive layers, while MDF uses binding agents to hold wood fibers together. These substances may generate additional smoke and emissions during laser processing.
A board marketed for woodworking is not automatically suitable for laser cutting. Review the manufacturer’s technical documentation and safety data before processing unfamiliar materials. Materials containing unsuitable coatings or chemical additives should not be introduced into the machine without confirming their compatibility.
How Thick Can a CO2 Laser Cut Wood?
There is no universal maximum cutting thickness for every CO2 laser cutter. The practical limit depends on laser output, wood species, density, moisture, focus position, and the required edge finish.
Thicker or denser boards generally require more processing energy. Higher laser power can help maintain cutting capacity, but it does not guarantee a clean edge or eliminate carbonization.
For commercial applications, buyers should evaluate three aspects:
- Cut-through performance:Can the machine completely cut the actual board without leaving uncut fibers?
- Edge quality:Is the amount of darkening or carbonization acceptable for the finished product?
- Production speed:Can the required cutting result be achieved at a practical operating speed?
Research published in the European Journal of Wood and Wood Products examined how laser beam power and feed rate affect the processing of different wood species. The findings reinforce that cutting results are influenced by both processing parameters and the characteristics of the wood itself.
A material test using the actual production board is therefore more reliable than choosing equipment based on a general thickness claim.
Which Machine Features Matter Most for Wood Laser Cutting?
A production-oriented wood laser cutter needs more than sufficient laser output. The working area, table design, motion system, and extraction setup all influence whether the equipment can support the intended workflow.
Does Laser Power Determine Cutting Performance?
Laser power determines the energy available for processing, but it must be matched to the material and production requirements.
Lower-power configurations may suit thinner materials, smaller components, and customized work. Higher-power configurations can be considered for thicker boards or workflows requiring greater cutting capacity.
However, excessive power or slow cutting speeds can increase heat accumulation and produce darker edges. Buyers should compare complete cutting results rather than assuming that the highest-power machine will always deliver the best finish.
Does the Working Table Affect Wood Cutting?
Yes. The working table supports the material and influences smoke movement beneath the cutting area.
A honeycomb table provides distributed support and can be useful for smaller components and detailed cutting layouts. A knife-strip table offers more open space beneath the cutting path, making it worth evaluating for larger or more rigid workpieces.
| Table type | Main advantage | Suitable applications |
| Honeycomb table | Distributed support for smaller parts | Decorative patterns and small components |
| Knife-strip table | Open space beneath the cutting path | Larger sheets and selected rigid workpieces |
The choice should reflect the workpiece dimensions, part geometry, and under-table smoke clearance. Material support and smoke removal should be considered together.
Why Are Air Assist and Fume Extraction Essential?
Air assist directs airflow toward the cutting area, helping clear smoke and debris around the laser path. Fume extraction removes contaminated air from the machine enclosure.
These functions are related but not interchangeable. Air assist does not replace a properly designed exhaust or filtration system.
Wood cutting can generate smoke, fine particles, and gaseous emissions. Engineered boards may also release substances associated with their adhesives and binders. Effective extraction, suitable ventilation, and regular filter maintenance are therefore important parts of the equipment setup.
Buyers should check the manufacturer’s extraction requirements, airflow capacity, duct arrangement, and filtration specifications. The system must be suitable for the materials being processed and the installation environment.
Does the Motion System Matter for Detailed Wood Parts?
Yes. A stable motion system helps maintain consistent movement along complex cutting paths. This is particularly important when producing repeated components, small openings, intricate patterns, or parts that need to fit together.
Rather than comparing machine components by name alone, evaluate positioning consistency and cutting performance using representative production files. The machine should reproduce the required geometry across repeated jobs without introducing unacceptable variation.
Which Industries Use CO2 Laser Cutting for Wood?
CO2 laser cutting is useful in industries where products require customized shapes, detailed contours, or repeatable decorative designs.
Furniture manufacturing uses laser cutting for selected decorative components, inserts, and panel details. It can support customized designs without requiring a different mechanical cutting tool for every pattern.
Signage and display production benefits from the ability to cut wooden letters, logos, signs, and display elements. Digital design files also make it easier to produce different versions for individual customers.
Craft and gift manufacturing uses laser cutting for personalized products, ornaments, and customized accessories. The process is suitable for small batches where product designs change frequently.
Interior decoration applications include patterned panels, decorative screens, and selected architectural details. The working area should accommodate the dimensions of the panels being processed.
Laser cutting is not automatically the most economical method for every wooden part. Simple shapes produced in very large quantities may be more efficiently manufactured through conventional woodworking processes. Laser equipment is particularly worth evaluating when design complexity, customization, and frequent design changes are important.
How Can MimoWork Support Wood Laser Cutting Applications?
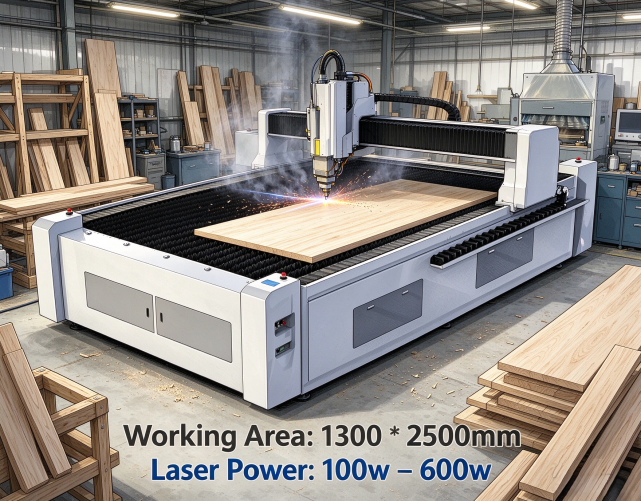
MimoWork offers CO2 laser equipment in different working-area and power configurations, allowing businesses to evaluate machine options according to their material dimensions and production requirements.
For smaller customized products and components, the F100 and F130 configurations provide different working areas. For larger sheet-based applications, the F130-L offers a larger working format for evaluation.
The selection should begin with the actual wood-processing requirements rather than the machine’s maximum power rating. Board dimensions, material composition, cutting thickness, part geometry, and expected production volume all influence the suitable configuration.
For businesses considering an industrial wood laser cutting machine, a practical evaluation should include representative wood samples and cutting files. This makes it possible to assess cut-through performance, edge condition, smoke removal, and processing consistency before confirming a production setup.
What Should You Check Before Buying a CO2 Laser Cutter for Wood?
A machine comparison should focus on whether the equipment can handle the actual production workflow.
| Evaluation point | Questions to ask |
| Material compatibility | Has the actual wood or board type been tested? |
| Cutting capacity | Can it cut the required thickness at a practical speed? |
| Working area | Does the bed fit the largest sheet and planned cutting layout? |
| Edge quality | Are the cut edges acceptable for the finished product? |
| Extraction | Does the exhaust setup meet the machine and material requirements? |
| Production workflow | Can the machine support the expected batch size and loading process? |
A sample test is especially valuable when working with plywood, MDF, or unfamiliar wood species. It helps identify material-related limitations before they affect production planning.
Frequently Asked Questions About CO2 Laser Cutting Wood
Can a CO2 laser cut plywood?
A CO2 laser can cut selected plywood products, but adhesive composition and board consistency affect the result. Check the material documentation and test the actual plywood before production.
Does laser-cut wood always have dark edges?
Some darkening or carbonization is common because laser cutting uses heat to remove material. Material selection, power, speed, focus, and airflow influence the final edge appearance. The goal is to control excessive burning rather than assume every wood type will produce a completely clean edge.
Is a CO2 laser cutter suitable for furniture production?
It can be suitable for decorative furniture components, patterned panels, and selected customized parts. The machine’s working area and cutting capacity must match the dimensions and materials used in the furniture workflow.
Is fume extraction necessary when cutting wood?
Yes. Wood cutting generates smoke and airborne contaminants that need to be removed from the machine enclosure. Use an extraction or filtration system suitable for the material and installation environment, and follow the equipment manufacturer’s safety requirements.
Can one CO2 laser machine handle both engraving and cutting?
Yes. A suitably configured CO2 laser machine can perform both processes. However, engraving and cutting require different processing parameters, and the machine must have sufficient capacity for the intended applications.
Select a CO2 Laser Cutter Based on Real Wood Samples
A suitable CO2 laser cutter for wood should match the material, workpiece dimensions, edge-quality requirements, and production volume. Laser power is only one part of that decision. Material compatibility, table design, motion stability, and fume extraction also affect the performance of the complete system.
Before choosing a machine, prepare the wood samples and cutting files used in your production. Contact MimoWork to discuss your required working area and configuration, and evaluate the cutting results on your actual material.
References
- Maciak, A. et al. — European Journal of Wood and Wood Products (2024). Effects of beam power and feed rate in the process of cutting fresh wood with a CO₂ laser on water contact angle on the cut surface.
2. MIT Environment, Health & Safety (2024). Laser Cutter Safety Guidance.