Blog
In a field that evolves daily, staying ahead means staying informed.
Explore in-depth articles designed to help you solve complex challenges,
maximize your machine’s ROI.
Stay ahead in a competitive market.


In a field that evolves daily, staying ahead means staying informed.
Explore in-depth articles designed to help you solve complex challenges,
maximize your machine’s ROI.
Stay ahead in a competitive market.
News | Nov-7-2026 | Mimowork
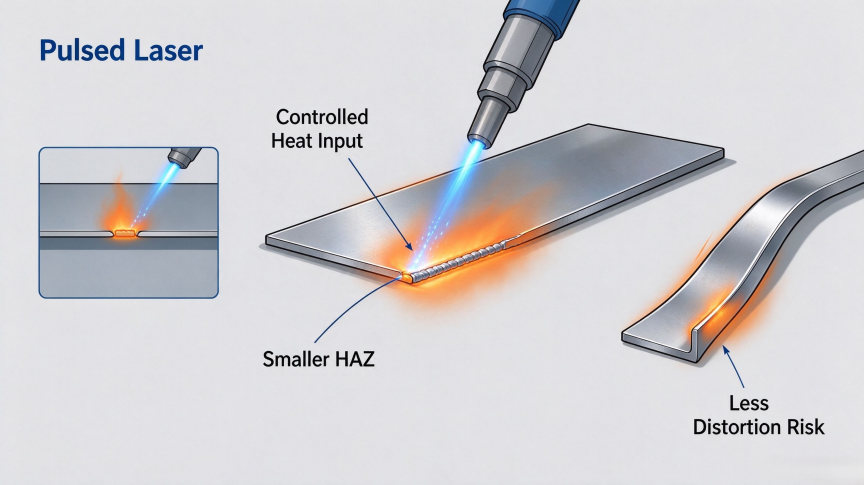
Pulse laser welding delivers energy in controlled bursts rather than maintaining a continuous beam. This allows the operator to adjust pulse energy, duration, and frequency to limit unnecessary heat input around the weld.
For thin metal sheets, small components, and localized repairs, this can reduce the risk of warping, burn-through, and excessive heat-affected zones (HAZ). However, it does not eliminate thermal distortion entirely. Material thickness, joint design, clamping, and parameter selection still determine the final result.
When a metal workpiece is heated, the material expands. During cooling, the weld zone contracts. If different areas cool and contract unevenly, residual stresses develop and the workpiece may bend or twist.
Traditional arc welding can expose a relatively large area to heat. Continuous laser welding concentrates energy more tightly, but the beam still delivers energy throughout the welding process. Excessive heat input or unsuitable welding speed can therefore create distortion even with a laser source.
Thin stainless steel sheets have limited material thickness to absorb and distribute heat. Excessive energy can cause edge deformation, burn-through, or uneven weld beads.
Dissimilar metals introduce another challenge: different thermal conductivity, melting temperatures, and expansion rates can make the weld pool difficult to control. A process that works well for one alloy combination may produce defects in another.
Distortion is not just a cosmetic problem. Warped parts may require straightening, grinding, refitting, or even complete rework.
These additional steps increase labor time and can affect dimensional accuracy. Reducing excessive heat input during welding can help lower the likelihood of these downstream costs.
A pulsed laser uses several adjustable parameters, including peak power, pulse energy, and pulse duration.
Peak power influences how much energy is delivered during the pulse and can affect penetration. Pulse duration influences how long the material remains exposed to the laser, affecting weld width and the amount of heat transferred into the surrounding material.
The goal is not simply to use the highest peak power. Excessive energy can cause spatter, porosity, or burn-through. A suitable combination of pulse energy and duration is more important than any single setting.
Between pulses, the laser temporarily stops delivering energy. During this interval, heat can conduct away from the immediate weld area.
This creates opportunities to control the thermal cycle instead of continuously heating the same region. However, the cooling effect depends on pulse frequency, pulse overlap, material properties, and the time between successive pulses. At high repetition rates, the workpiece may still experience substantial heat accumulation.
The concentrated energy delivery can help restrict melting to the intended weld area and reduce unnecessary heating around it.
A smaller heat-affected zone can be beneficial for thin components and precision assemblies. However, the actual HAZ size is not automatically measured in micrometers or guaranteed to be smaller in every application. It must be evaluated through weld trials and metallographic inspection when dimensional or material properties are critical.
Thin stainless steel and titanium components can benefit from carefully controlled laser pulses, particularly when the joint requires localized heating and limited distortion.
For sheets around 0.5–2 mm, the appropriate process depends on the exact alloy, joint geometry, fit-up, and required penetration. This thickness range should be treated as an application to test, not a universal capability of every pulsed laser welder.
Titanium also requires suitable shielding to prevent oxidation and contamination during welding.
Small enclosures, sensor housing, and precision metal components often have limited space for heat management. Excessive heat may damage nearby parts or affect dimensional tolerances.
Pulsed energy can provide localized control for small welds and delicate assemblies. For medical devices and other safety-critical components, however, weld strength, hermeticity, cleanliness, and process repeatability must be verified against the relevant product and industry requirements.
Pulsed laser technology can be used in specialized mold-repair processes where a small amount of material must be added to a localized damaged area.
The operator must control pulse energy, filler material, and heat input to avoid damaging the surrounding tool steel. Whether a particular system can perform this work depends on its laser source, pulse characteristics, optical setup, and repair procedure. A jewelry-focused pulsed welder should not automatically be assumed suitable for industrial mold restoration.
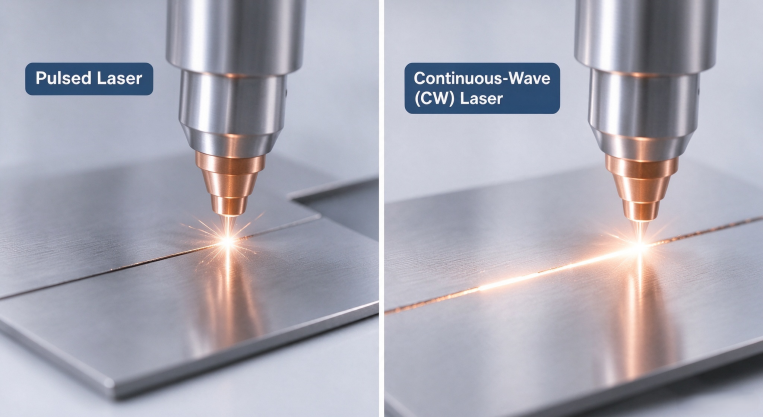
Neither output mode is universally better. The right choice depends on the workpiece thickness, required penetration, joint geometry, and production speed.
| Selection Factor | Pulsed Laser | Continuous-Wave (CW) Laser |
| Energy delivery | Intermittent pulses | Continuous output |
| Heat control | Adjustable pulse energy and duration | Controlled mainly through power, speed, and beam characteristics |
| Typical advantage | Localized welding and precision work | Stable energy delivery and deeper penetration in suitable applications |
| Suitable work | Small components, thin sections, localized repairs | Structural parts, longer seams, and thicker materials |
| Main consideration | Pulse overlap and heat accumulation | Total heat input and welding speed |
For pulse laser welding, the main advantage is the ability to adjust the energy delivered to each weld location. CW systems are often more suitable when higher average power, continuous seams, or greater penetration are required.
A practical selection rule is straightforward: choose a pulsed system when localized energy control is the priority; consider CW when penetration, seam continuity, and production throughput are more important. Test samples from the actual material and joint design before making the final decision.
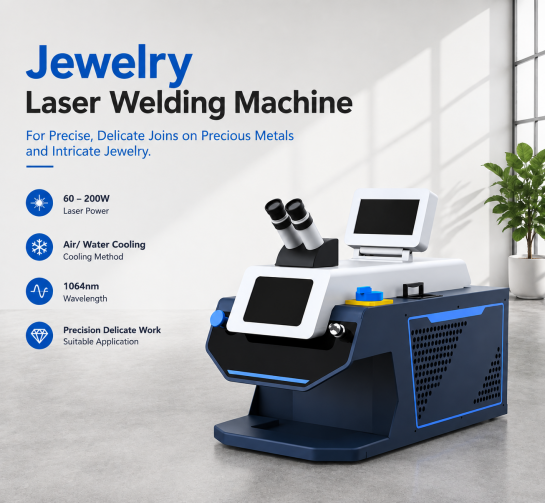
MimoWork offers a Jewelry Laser Welding Machine designed for delicate joining and repair work on precious metals.
Its published specifications include:
| Parameter | MimoWork Jewelry Laser Welding Machine |
| Laser source | Pulsed fiber |
| Laser power | 60–200W |
| Wavelength | 1064nm |
| Cooling | Air or water cooling |
| Application | Precision, delicate work |
The machine combines a micro-pulse fiber laser source with a microscope and fine-focus welding head. Adjustable pulse controls allow operators to tune pulse energy and duration for small welds. An argon gas system is also available to help protect precious metals from oxidation during processing.
These features are relevant to jewelry repair, prong retipping, chain repair, and intricate metal assembly. They are not a blanket guarantee of suitability for every industrial sheet-metal or mold-repair application.
Explore the MimoWork Jewelry Laser Welding Machine to review its configuration and application details.
They can achieve strong joints when the material, joint design, and welding parameters are properly matched. However, strength cannot be determined by the laser mode alone.
Penetration depth, fusion quality, porosity, cracking, and the effective weld area all influence joint performance. Tensile, shear, or other application-specific tests are needed to establish whether a weld meets the required standard.
Pulse energy affects the amount of energy delivered in each burst, while pulse frequency determines how often those bursts occur.
Higher pulse energy may increase penetration but can also increase the risk of burn-through and spatter. Higher frequency can create more overlap between pulses and may increase heat accumulation. Operators should adjust these parameters together rather than changing one setting in isolation.
Many metal welding applications use shielding gas to protect the molten weld pool from atmospheric contamination.
Argon is commonly used for materials such as stainless steel and titanium, although the appropriate gas and flow conditions depend on the material and process. MimoWork’s jewelry welding system includes an argon gas inerting system for protecting precious metals during welding.
It depends on the laser source and its output mode, not simply whether the machine is handheld.
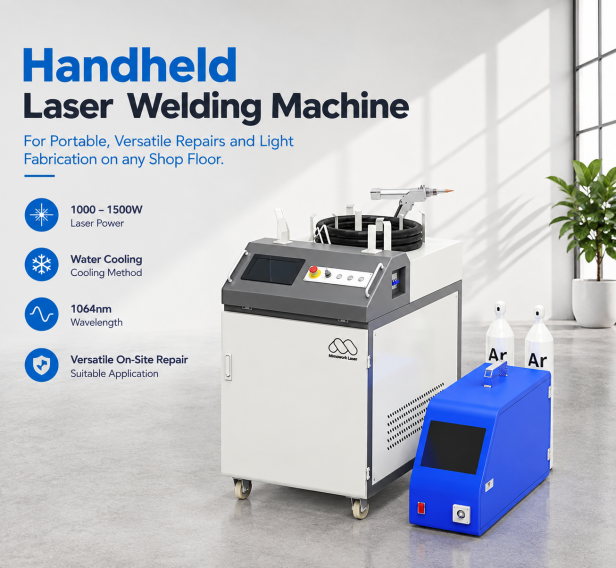
MimoWork’s handheld laser welding machines are listed separately from its 60–200W pulsed jewelry welding system. The handheld range uses higher-power fiber laser configurations for fabrication and repair applications. For thick structural components, penetration requirements, joint preparation, and the machine’s actual power configuration must be evaluated before selection.
Welding distortion often begins with excessive or uneven heat input. Controlling energy delivery can reduce the risk of warping, burn-through, and unnecessary post-weld correction.
Pulsed systems are worth considering for thin sections, small components, and precision repairs where localized heat control matters. For thicker parts and continuous structural seams, CW systems may offer a more practical balance of penetration and productivity.
The best choice comes from matching the laser source and process parameters to the actual material, joint, and quality requirements—not from choosing a higher power rating alone.
Related guide:Laser Welding vs. Arc Welding for Thick Steel: Which Is More Efficient?
News | Oct-30-2026