Blog
In a field that evolves daily, staying ahead means staying informed.
Explore in-depth articles designed to help you solve complex challenges,
maximize your machine’s ROI.
Stay ahead in a competitive market.


In a field that evolves daily, staying ahead means staying informed.
Explore in-depth articles designed to help you solve complex challenges,
maximize your machine’s ROI.
Stay ahead in a competitive market.
News | Oct-31-2026 | Mimowork
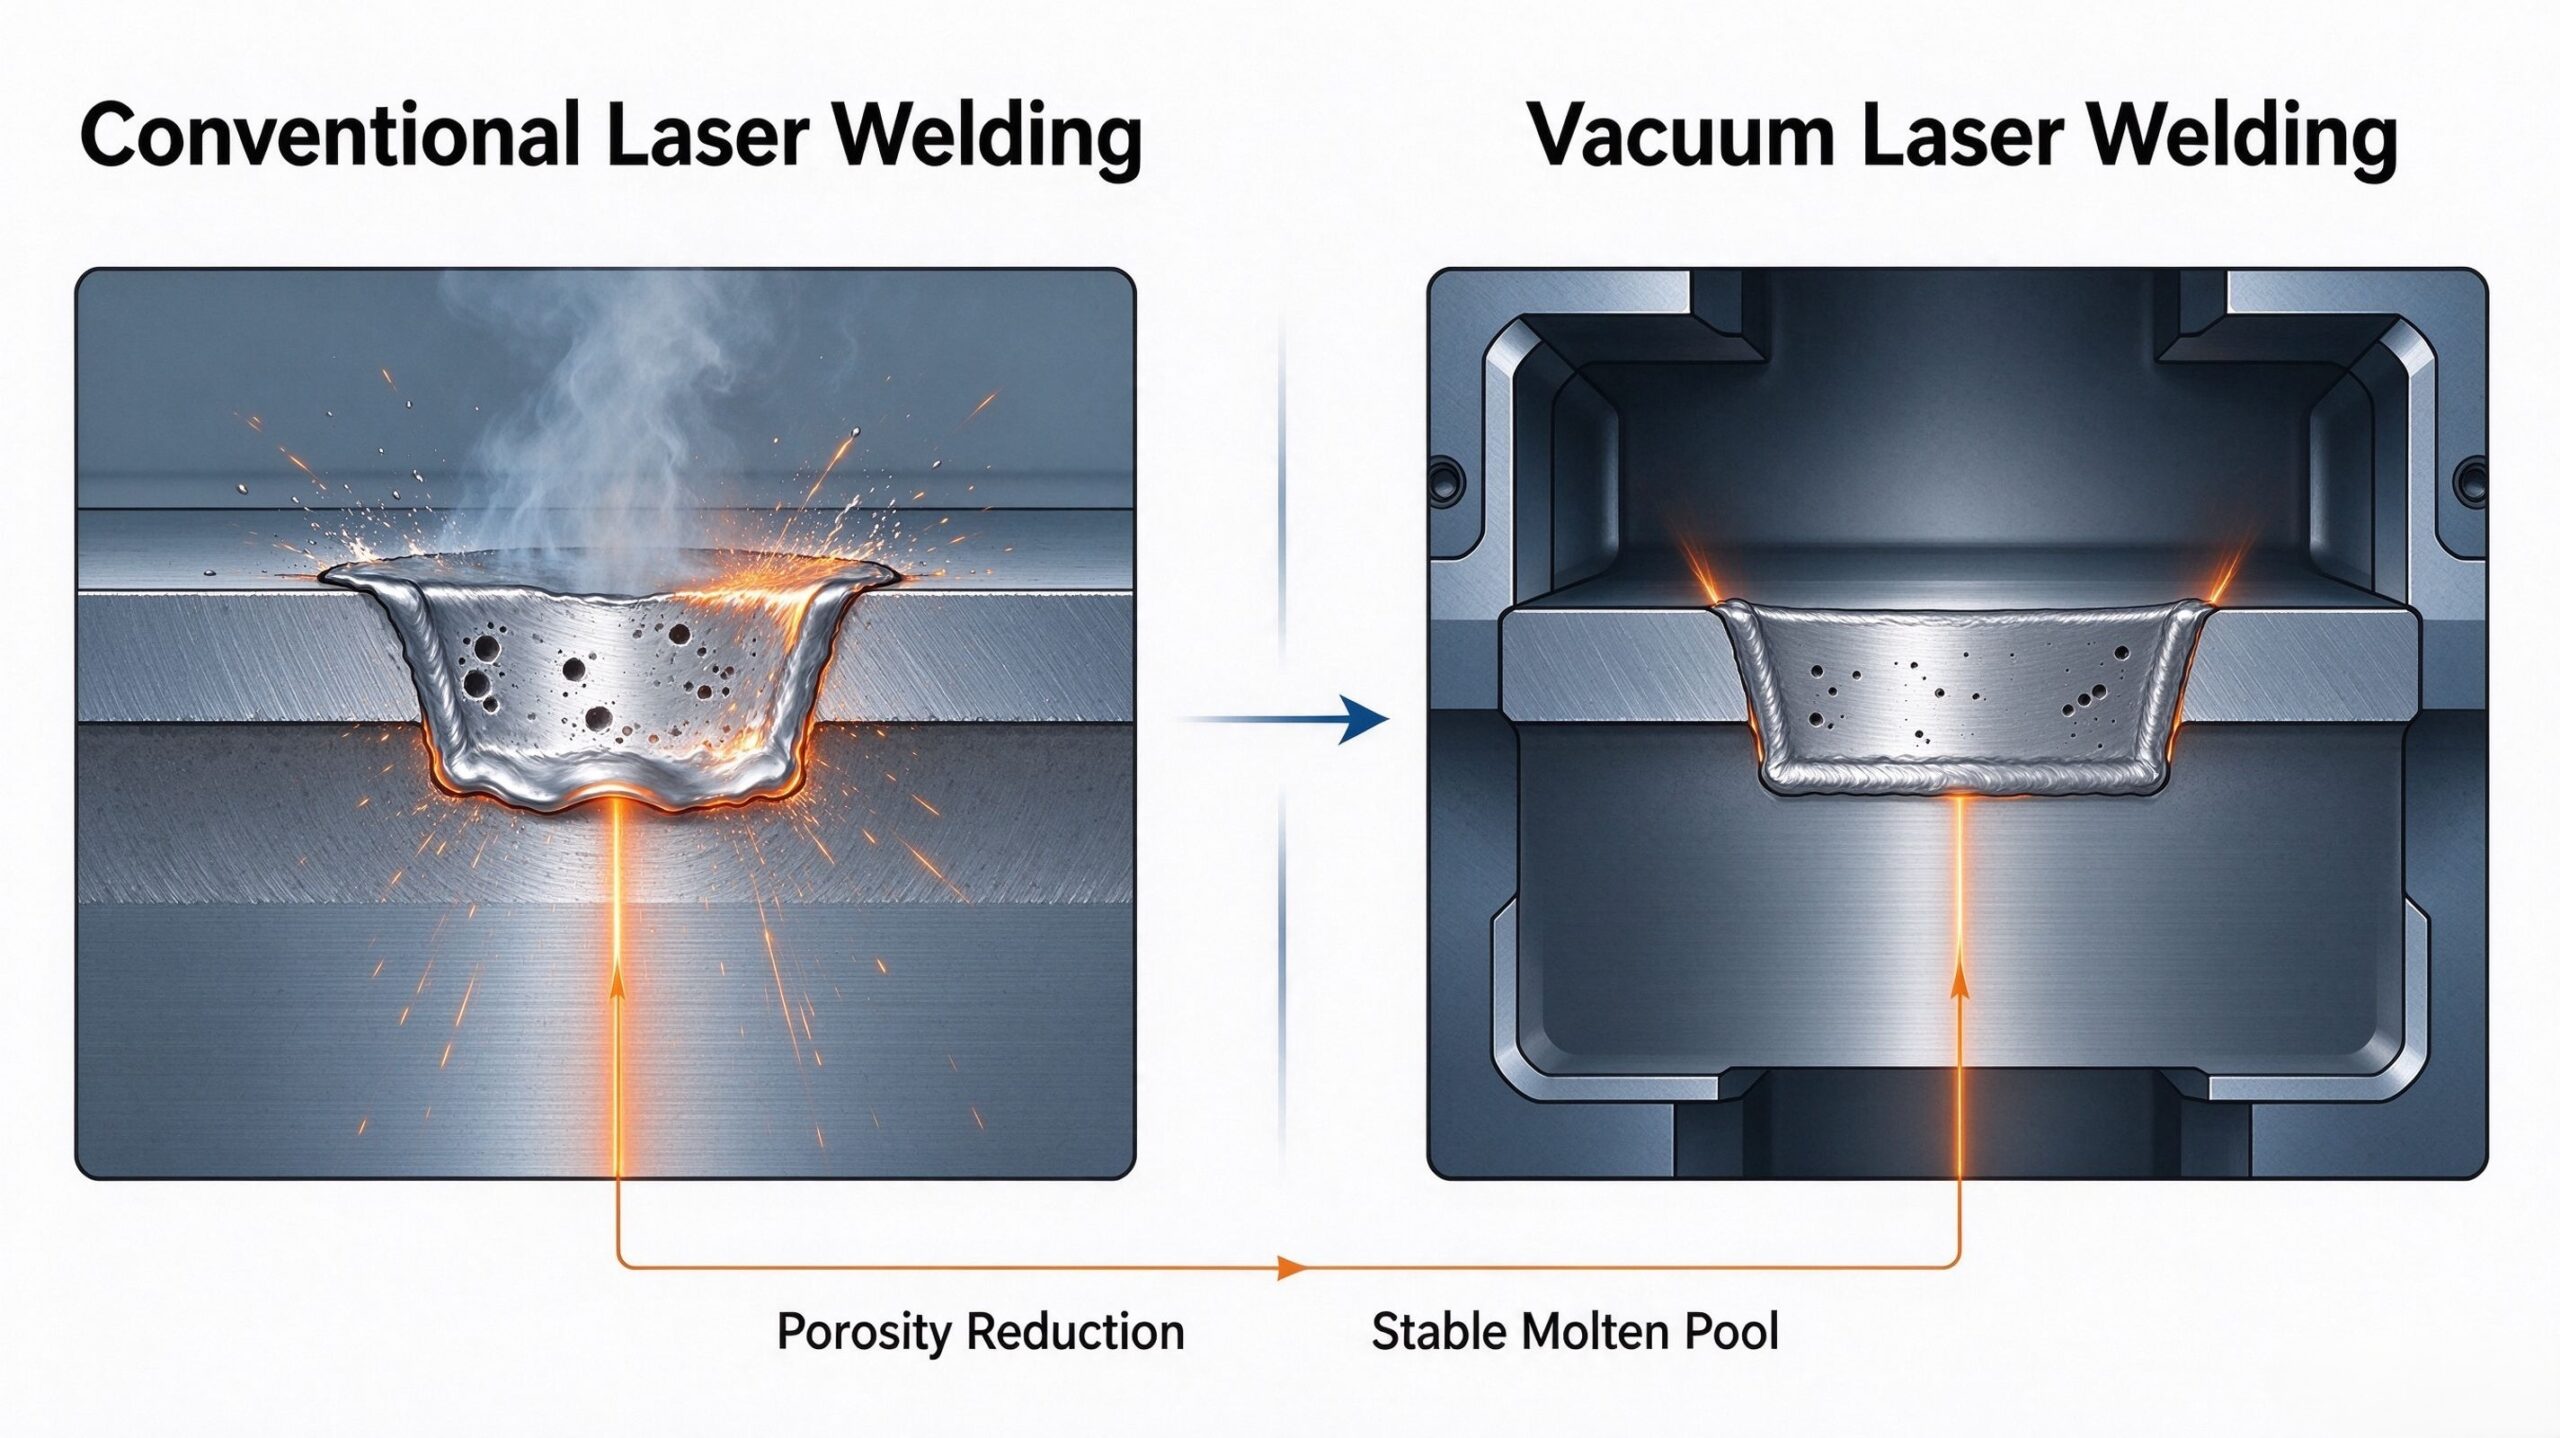
Vacuum laser welding uses a focused laser beam to join metal components inside a vacuum or reduced-pressure environment. Lower ambient pressure can improve penetration and reduce certain weld defects, including porosity, under suitable material and process conditions. However, the process requires a vacuum chamber, pressure-control equipment, and a production workflow that accommodates chamber loading and evacuation. It is most worth evaluating when weld quality, penetration depth, or defect control justifies the additional equipment and cycle time.
A weld can look acceptable on the surface while containing internal pores or an inconsistent fusion zone. These defects can become expensive when components must meet strict mechanical, dimensional, or quality requirements. Reworking a finished assembly is particularly difficult when the weld is inaccessible or the component has a high material value.
Conventional laser welding already offers concentrated energy input and precise control. However, some materials and joint configurations remain challenging because of vapor formation, unstable keyholes, trapped gas, or spatter.
Vacuum processing changes the environment in which the weld forms. Reducing ambient pressure affects metal vapor behavior, the laser-induced plume, and the stability of the molten pool. Research has reported improvements in penetration and certain defect characteristics under suitable conditions, although the results depend on the material, pressure level, joint design, and process parameters.
For manufacturers, the important question is not simply whether vacuum improves a weld. It is whether the improvement addresses a costly problem in the actual production process.
The basic principle is similar to conventional laser beam welding: a focused laser beam delivers energy to the joint, melts the base material, and forms a weld as the molten metal solidifies. The difference is the controlled-pressure environment surrounding the workpiece.
A typical process involves three stages.
1. Prepare and position the components. The workpieces are cleaned, aligned, and secured in a fixture. Joint fit-up remains important because vacuum conditions do not eliminate gaps, contamination, or poor component preparation.
2. Establish the required pressure. The components are placed inside a vacuum chamber, which is evacuated to the target pressure for the application. The required pressure depends on the material and process; not every application requires the same vacuum level.
3. Apply the laser and verify the weld. The laser follows the specified welding path while the process is controlled according to the material, joint geometry, and quality requirements. Weld inspection then determines whether the process achieves the required penetration, geometry, and internal quality.
The chamber and its associated systems are part of the process, not optional accessories. Their size, pumping capacity, access arrangements, and compatibility with the laser system all influence production practicality.
Reduced ambient pressure can change the behavior of metal vapor and the laser-induced plume, allowing deeper penetration in certain applications. This may be valuable when a component requires a relatively deep weld without an excessively wide surface bead.
Actual penetration still depends on laser power, beam characteristics, travel speed, material properties, and joint design. Vacuum alone does not guarantee a deeper or stronger weld.
Porosity is a major concern when gas becomes trapped in the molten metal during solidification. In some materials, reducing the surrounding pressure can help alter the conditions that contribute to pore formation.
However, the effect is not universal. Research on high-pressure die-cast aluminum, for example, identifies trapped hydrogen as an important contributor to weld porosity. The starting material and its gas content therefore remain important even when welding under reduced pressure.
Manufacturers should validate weld quality through appropriate inspection rather than assume that a vacuum chamber eliminates internal defects.
Lower ambient pressure can influence the laser-induced plume, vapor flow, and molten-pool behavior. Under appropriate conditions, these changes may reduce spatter and improve process stability.
The practical benefit may include less surface contamination and less cleanup. Nevertheless, fixture design, surface preparation, laser parameters, and material characteristics continue to affect the result.
Applications involving strict internal quality requirements, deep penetration, or difficult-to-weld materials may justify evaluating a vacuum process. The decision should be based on demonstrated weld performance and production economics, not on the assumption that vacuum is inherently superior for every metal component.
Vacuum welding is not automatically the best choice for every factory. Its value is greatest when the component’s quality requirements justify the chamber and process-control requirements.
| Application area | Potential reason to evaluate vacuum welding | Key consideration |
| Automotive cast components | Controlling porosity in selected cast aluminum parts | Alloy condition, gas content, and joint design |
| Aerospace and high-performance components | Achieving demanding weld quality or penetration requirements | Material qualification, inspection, and process repeatability |
| Precision metal assemblies | Improving consistency for selected complex joints | Fixture accuracy and component fit-up |
| Research and specialized manufacturing | Studying or controlling weld formation under reduced pressure | Pressure control, process monitoring, and validation |
These are potential application areas rather than a guarantee that every component in an industry needs vacuum welding. A representative weld trial should establish whether the process delivers a meaningful improvement over conventional laser welding.
The main difference is the processing environment and the equipment required to maintain it. The right choice depends on the production problem being solved.
| Comparison factor | Vacuum laser welding | Conventional laser welding |
| Processing environment | Vacuum or reduced-pressure chamber | Usually atmospheric conditions, with shielding gas where required |
| Penetration behavior | May achieve greater penetration under suitable conditions | Depends on laser parameters and material behavior |
| Porosity control | Can reduce certain porosity mechanisms in suitable applications | Depends on material, joint design, preparation, and process control |
| Equipment requirements | Laser system plus chamber and vacuum equipment | Laser system with suitable fixtures and process auxiliaries |
| Production flexibility | Limited by chamber size, loading, and evacuation cycles | Often easier to integrate into open or continuous production workflows |
| Best selection criterion | A demonstrated need for vacuum-related process benefits | Reliable weld quality without the additional vacuum infrastructure |
For many manufacturers, conventional laser welding remains the more practical choice when the parts can be welded reliably under atmospheric conditions. Vacuum equipment introduces additional capital cost, maintenance, and cycle-time considerations that must be justified by the resulting quality improvement.
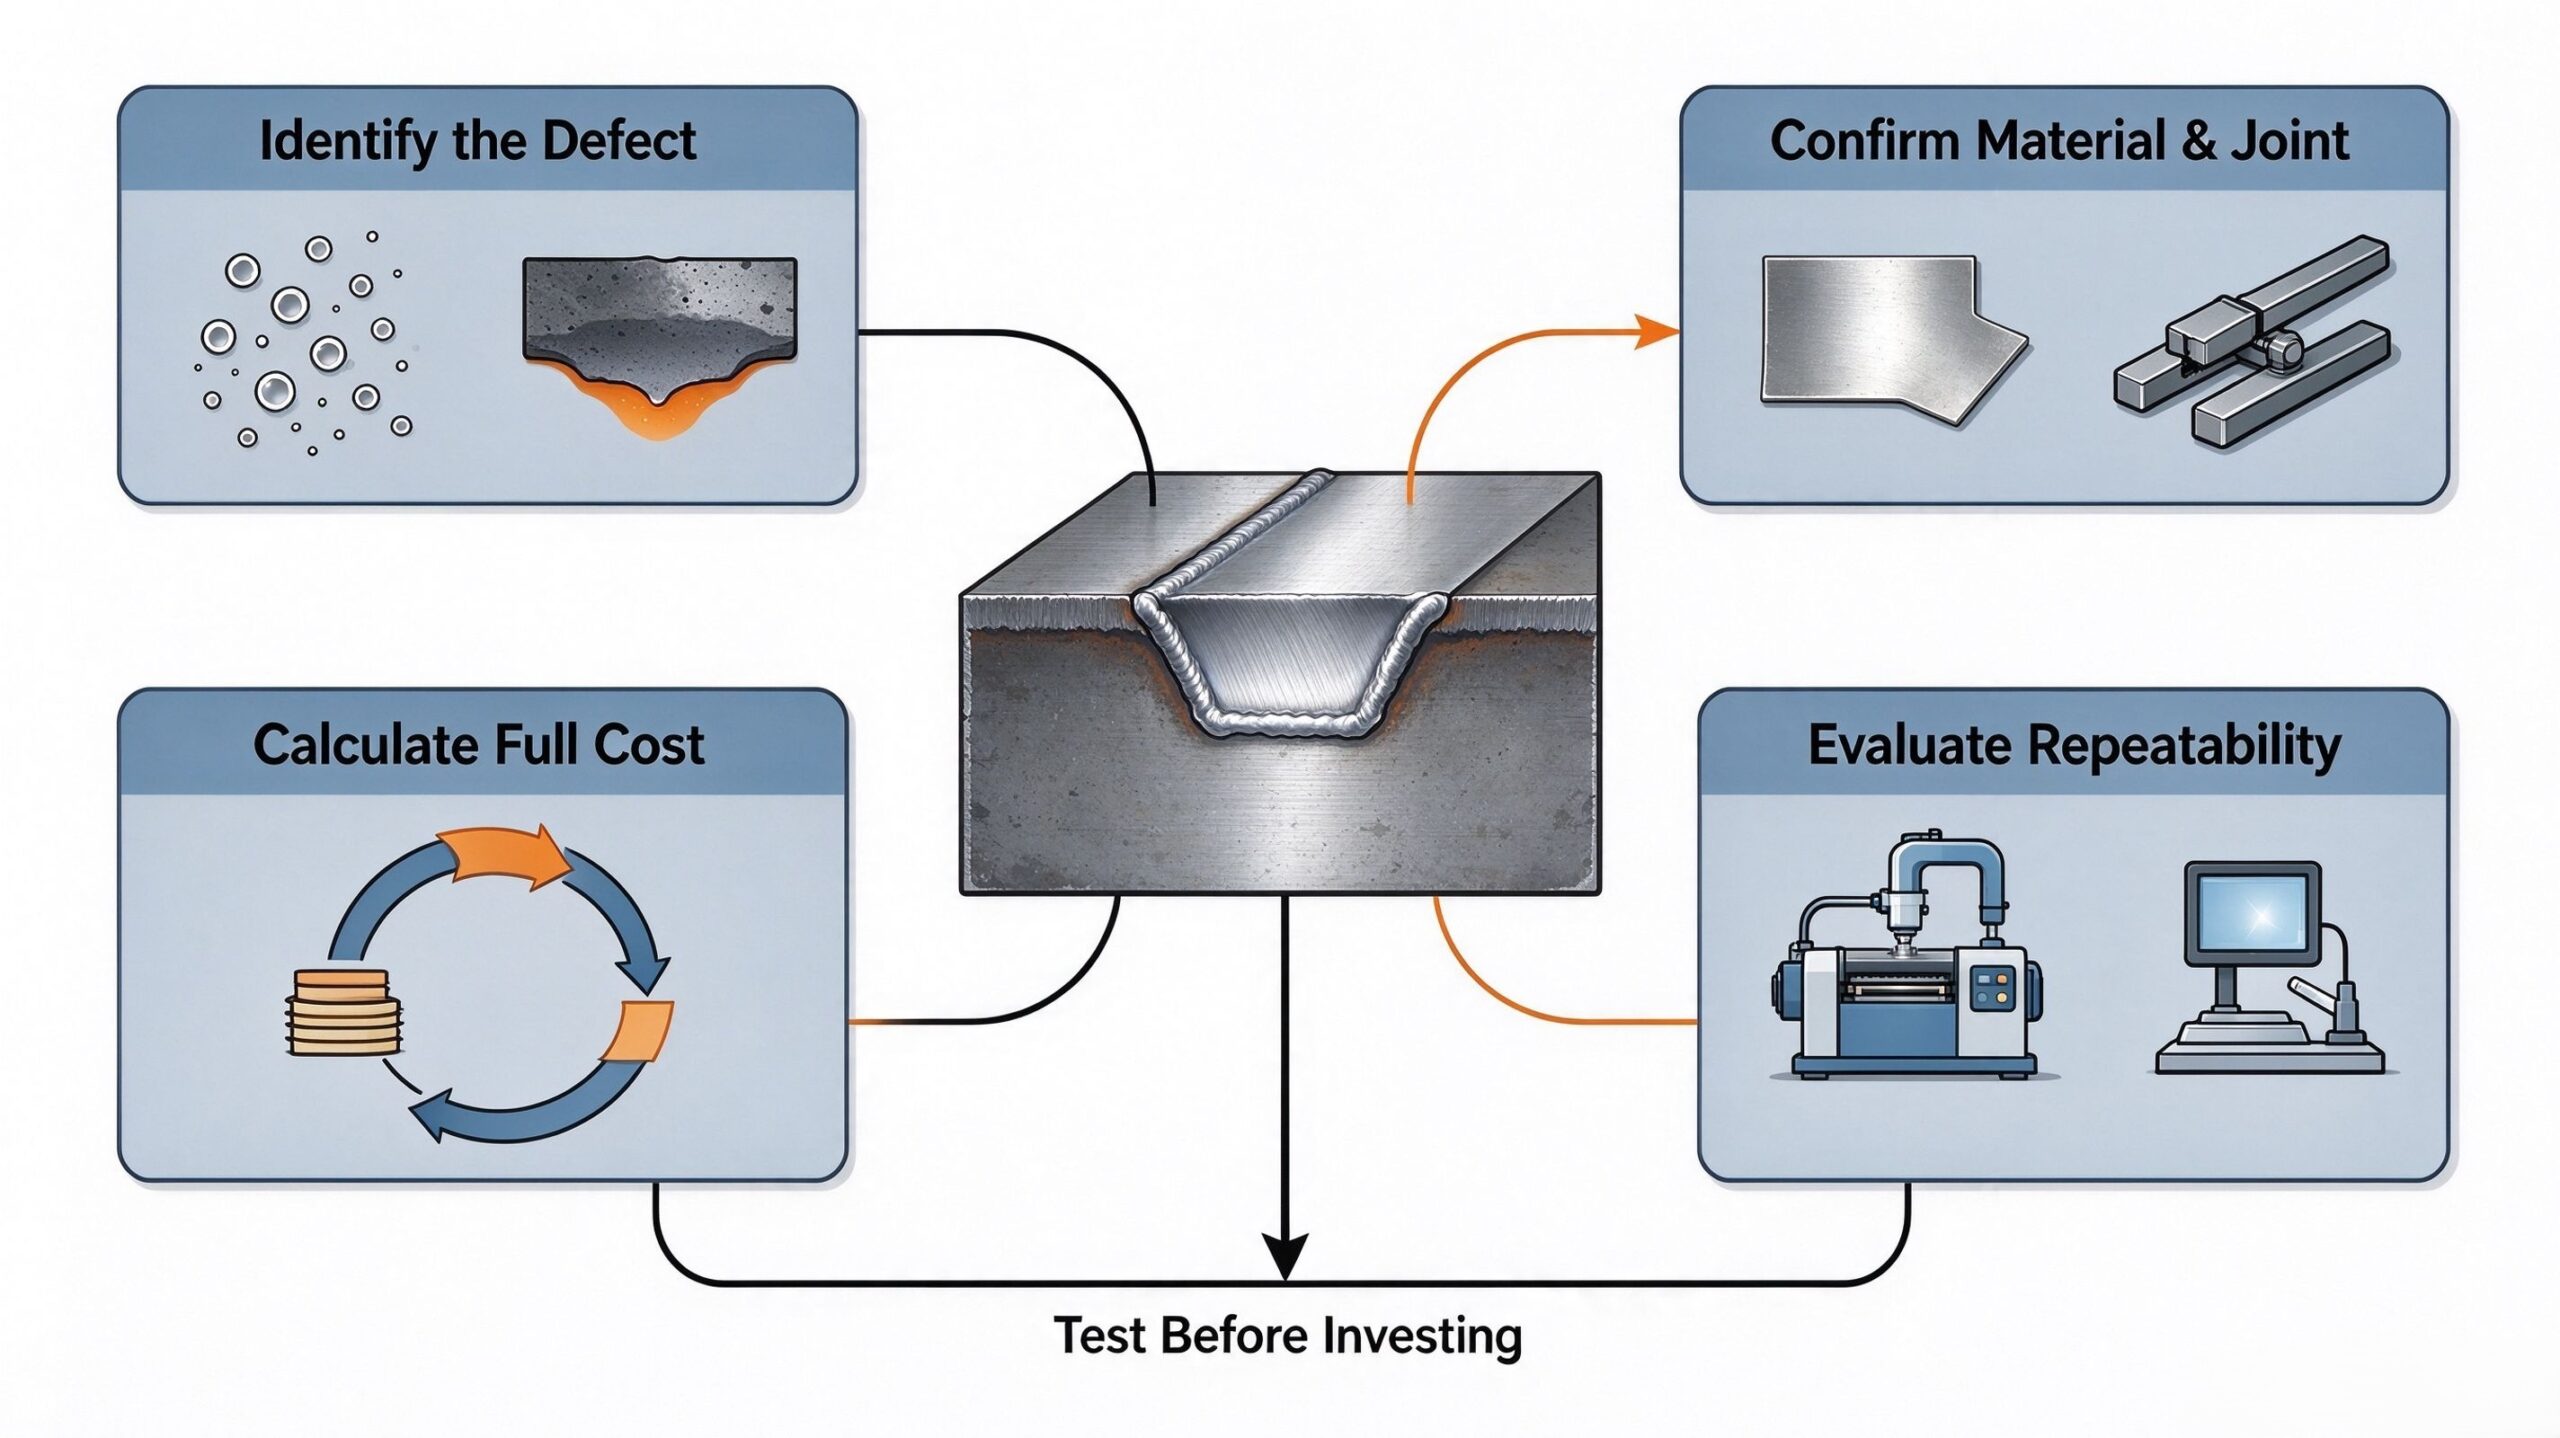
Identify the actual problem: internal porosity, insufficient penetration, excessive spatter, inconsistent weld geometry, or another quality issue. These defects can have different causes, and some may be addressed through material preparation, joint design, fixturing, or parameter adjustments without introducing vacuum processing.
The same pressure conditions may produce different results across alloys and joint configurations. Material thickness, surface condition, trapped gas, joint gap, and the required weld geometry all affect process performance.
Provide the equipment supplier with representative parts and clear acceptance criteria. A useful test should evaluate the defect that matters to your production process, not just the appearance of the weld bead.
The investment is not limited to the laser source. Consider the chamber, vacuum pumps, fixtures, loading and unloading, maintenance, inspection, and the time required to reach the target pressure.
Compare the expected reduction in scrap and rework with the added cost per part. A process that improves weld quality but creates a bottleneck in production may not be the most economical solution.
For recurring production, assess how components enter and leave the chamber, how fixtures maintain alignment, and how welding parameters are controlled. Repeatable loading and reliable process monitoring can be just as important as the laser itself.
Related guide:Aerospace Laser Welding: Applications, Materials, and How to Choose the Right Systems
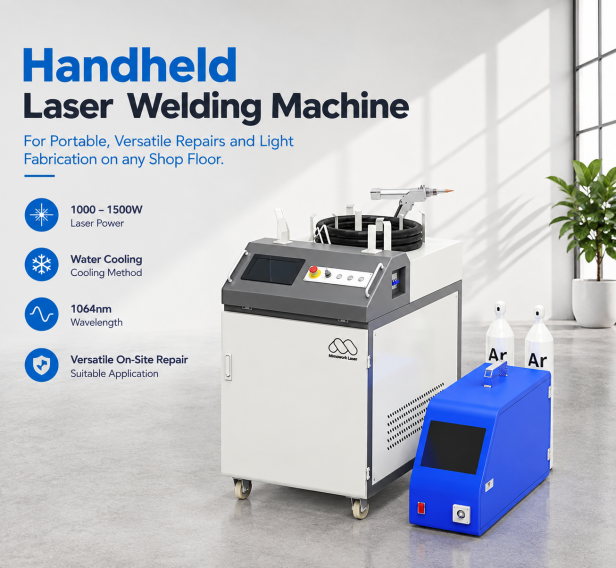
Choosing a laser welding solution starts with understanding the material, joint design, and weld quality your application requires. For manufacturers exploring vacuum laser welding, factors such as penetration depth, porosity control, and process consistency can help determine the most suitable welding approach.
MimoWork offers a range of Laser Welding Machine solutions for metal fabrication, repair, jewelry manufacturing, and other specialized applications. By discussing your workpiece materials, production requirements, and target weld quality with our team, you can identify a suitable equipment configuration and determine the process requirements for your application.
Whether you are evaluating vacuum-assisted welding or a conventional laser welding process, matching the equipment to your actual production needs is the first step toward achieving reliable weld quality.
No. It can reduce certain sources of porosity under suitable conditions, but results depend on the material, trapped gas, joint configuration, and process parameters. Weld inspection and application testing are still necessary.
Not for every application. Vacuum processing may offer advantages in penetration and defect control, but it requires additional equipment and can increase cycle time. Conventional laser welding is often more practical when it already meets the required quality standard.
Research has examined materials including aluminum alloys, copper, steel, and magnesium alloys. Suitability depends on the specific alloy, component geometry, joint design, and target weld properties. A material-specific trial is needed before production.
A standard handheld system is not automatically suitable for vacuum welding. The process requires a compatible chamber, pressure-control equipment, and a laser configuration designed for the intended setup. Confirm these requirements with the equipment supplier.
Vacuum welding can be valuable when conventional laser welding struggles with specific penetration or defect-control requirements. Its benefits must be demonstrated on the actual material and joint, then weighed against chamber costs, evacuation time, and production constraints.
For manufacturers evaluating their next welding system, the first step is to define the weld-quality problem and validate the process on representative components. MimoWork’s laser welding team can help discuss conventional laser welding applications and equipment requirements; applications that specifically require vacuum operation should be confirmed separately with the supplier.
News | Oct-30-2026
News | Oct-20-2026